Instrument Spotting After Sterilization: Water Quality Guide
Learn what white spots, rust-colored film, and dull haze suggest, which water tests to order, and when to hold, investigate, and reprocess a tray.
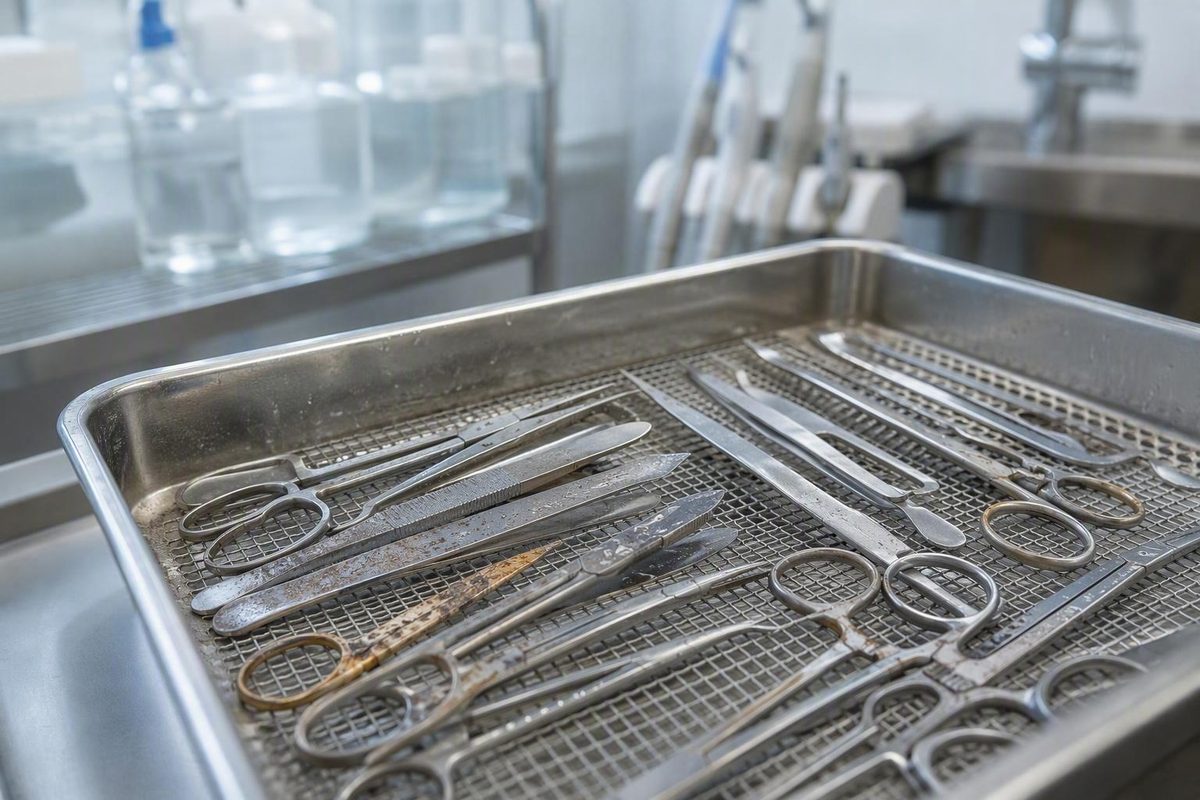
Freshly processed instruments with unexplained spots, film, or haze should not be wiped and released for use. Control the tray under facility policy, document the finding, and determine whether the residue began during washing, final rinsing, drying, or steam exposure. A wet, torn, or punctured package must not be used. Pitting, roughness, blocked lumens, impaired movement, or other surface damage requires technical evaluation rather than routine wiping.
Select the mark, location, removability, and first affected stage to see the likely cause, test, and tray action.
This tool ranks a process hypothesis; it does not identify a contaminant or authorize release. Select what you observed before anyone removes the evidence.
Test first: Hardness and conductivity at the actual final-rinse outlet; verify chemistry dosing and rinse performance.
Trace next: Compare treatment output with the washer outlet and inspect broad surfaces for a rack-position pattern.
Tray action: Control the tray under facility policy. Do not wipe and release it; document the deposit and use the approved disposition or reprocessing route.
| Observed Pattern | Leading Hypothesis | Parameter or Check | Disposition Signal |
|---|---|---|---|
| White Removable, after rinse or drying | Calcium or magnesium hardness; dried salts; chemistry residue | Hardness, conductivity, detergent and neutralizer dosing, rinse coverage | Hold; do not wipe-and-release; approved reprocessing or disposition |
| Clear/haze Broad water rings | Dissolved solids concentrated during drying | Conductivity at treatment output and final-rinse outlet; drainage and drying | Hold and define affected equipment or load pattern |
| Clear/haze Adherent film | Retained detergent, neutralizer, lubricant, soil, or mineral scale | Dosing calibration, spray coverage, cleaning verification, conductivity | Reprocess through approved route; no local wipe-down |
| Brown/rust Raised or removable | Iron-containing deposit or steam/distribution corrosion product | Iron and relevant metals; chloride; piping, chamber, and condensate review | Hold tray; preserve evidence before cleaning representative items |
| Brown/rust Pitted or rough | Corrosion or passive-surface damage | Chloride and relevant chemistry; magnified material assessment | Remove affected instrument for qualified technical evaluation |
| Blue/rainbow On mixed metals or contacts | Chemistry interaction, galvanic effect, metal deposition, or heat-related change | Material identification, mixed-metal contact, chemistry concentration, condensate | Hold and obtain instrument-specific assessment if adherent |
| Joint/lumen Residue or discoloration | Retained soil, inadequate flushing, mineral or chemistry deposit, corrosion | Validated internal inspection, flow and connector checks, rinse quality | Do not rely on exterior wiping; reprocess and evaluate function |
| Pooled area After drying | Drainage or orientation concentrating dissolved material | Loading, orientation, set design, conductivity, hardness, drying performance | Hold affected load and correct the process before release |
| Shared pattern Instruments plus wraps or chamber | Common steam, chamber, carryover, or drainage source | Point-of-use condensate, feedwater, boiler history, filters, traps, chamber | Control related loads according to the defined equipment and time window |
| After cleaning Before final rinse | Cleaning chemistry, retained soil, spray failure, or washer deposits | Dosing, cleaning verification, spray arms, rack connections, washer condition | Do not advance the tray; correct cleaning and repeat approved processing |
| After steam Absent before packaging | Steam carryover, boiler treatment, piping corrosion, chamber deposit; earlier residue still possible | Condensate chemistry, feedwater, chloride and metals as indicated, steam system review | Hold load and compare the same items before and after steam |
| Any color Wet, torn, or punctured package | Package-integrity failure handled separately from spot diagnosis | Package, drying, load configuration, cycle and equipment review | Do not use the package |
| Any color No visible damage but unexplained residue | Water, chemistry, soil, material, or process source remains unresolved | First affected stage plus targeted point-of-use testing | Control under policy; appearance alone cannot authorize release |
| Endotoxin Concern based on use or excursion | Pyrogenic risk requiring analytical assessment | Applicable endotoxin method and point-of-use sample | Visual appearance cannot clear or condemn on endotoxin grounds alone |
Source note: Decision logic is based on the article’s cited AAMI, CDC, manufacturer, and technical guidance. No numerical water-quality limits are reproduced; use current primary standards and applicable instructions.
Appearance Narrows the Investigation but Does Not Diagnose It
A visible spot is a symptom, not proof of a particular contaminant, treatment failure, sterilization failure, or microbial event. Water can carry calcium, magnesium, dissolved salts, metals, and treatment chemicals. Processing chemistry and inadequately removed soil can also remain on a device.
Heating and drying may concentrate dissolved material or cause it to precipitate. A deposit laid down during washing or rinsing may therefore become visible only after steam exposure. Contaminants can also enter through boiler feedwater, a steam generator, distribution piping, or the sterilizer chamber. An AAMI journal review of processing-water quality illustrates how chemical residuals become apparent when water is heated and dried.
Classify the finding before assigning a cause. A spot is generally a loose or semi-adherent deposit that may wipe away with minimal friction. A stain is more tightly adherent or appears integral to the surface. Pitting, cracking, roughness, flaking, or material loss suggests corrosion or physical damage rather than a simple deposit, as described in this technical overview of spotting, staining, and corrosion.
| Observation | Leading Possibilities | First Checks | Key Limitation |
|---|---|---|---|
| White or chalky residue | Hardness minerals, dried salts, chemistry residue | Hardness, conductivity, dosing, rinse performance | Color does not identify composition |
| Clear rings or dull haze | Dissolved solids, detergent or neutralizer residue | Conductivity, rinse supply, drainage, drying | Shape does not identify the source |
| Brown or rust-colored film | Iron deposit, corrosion product, chloride-related attack, carryover | Removability, pitting, iron, chloride, steam pathway | Brown does not prove the instrument is rusting |
| Blue or rainbow color | Chemistry interaction, metals, heat or galvanic effect | Materials, mixed-metal contact, dosing, condensate | Color charts are not definitive |
| Adherent film | Baked chemistry, soil, mineral scale, surface alteration | Cleaning, spray coverage, chemistry, water tests | Inspection cannot separate all residues |
| Roughness or pits | Corrosion, passive-layer damage, chemical attack | Magnified inspection and technical evaluation | Wiping cannot establish surface integrity |
White, chalky material is compatible with calcium or magnesium precipitation, particularly when it wipes away. Chlorides, sulfates, metals, retained chemistry, and surface damage belong in the differential for discoloration or corrosion. Manufacturer guidance likewise treats appearance as a reason to investigate, not as a laboratory identification (Aesculap’s water-quality overview).
Record whether the mark transfers to an approved wipe, but do not improvise with abrasives or unapproved chemicals. Note whether it is powdery, smooth, raised, crusted, rough, or pitted. Record its exact location, including box locks, serrations, lumen openings, tips, contact points, and areas where water can pool.
“It wiped off” establishes only that the visible material was removable. It does not establish that the instrument is clean, undamaged, functional, or ready for use.
The First Affected Stage Locates the Likely Source
Inspect representative instruments at controlled points in the process whenever the validated workflow permits:
- After cleaning and before the final rinse
- After the final rinse
- After drying and before packaging
- After the sterilization cycle
Use equivalent instruments or controlled test loads if intermediate inspection would conflict with safety requirements, equipment instructions, or validated workflow.
Marks Present Before Sterilization Point Toward Washing and Rinsing
A finding present after cleaning directs attention to detergent selection and dilution, chemistry delivery, manual technique, soil removal, lumen flushing, spray-arm operation, rack connections, washer scale, and intermediate-rinse performance.
A mark first seen after the final rinse makes the actual final-rinse outlet a priority. Check the supply under operating conditions rather than relying only on a sample from the treatment skid. Also review rinse coverage, valves, equipment piping, loading, and dosing of neutralizer or lubricant where applicable.
A mark that appears only after drying may represent dissolved material concentrated by evaporation. That pattern still cannot distinguish water minerals from chemistry residue, retained soil, or material released from the device surface.
Marks First Seen After Steam Expand the Search
If instruments are unmarked after final rinsing and drying but change after steam exposure, prioritize sterilizer or steam-generator feedwater, point-of-use condensate, boiler treatment, blowdown and maintenance, filters, traps, separators, regulators, distribution piping, carryover, chamber deposits, drainage, and drying.
Do not eliminate the final rinse. Heat may reveal residue that was deposited earlier. Conversely, similar staining on wraps, liners, racks, chamber surfaces, and several instrument materials supports investigation of a shared steam or chamber source without identifying the contaminant.
Condensate purity and steam quality answer different questions. Condensate testing evaluates chemical impurities delivered through the steam pathway. Actual steam quality concerns the physical suitability and performance of the steam, including dryness and system operation. A STERIS standards overview distinguishes processing-water and condensate-purity concerns under ANSI/AAMI ST108 from steam-sterilization and actual-steam-quality concerns under ANSI/AAMI ST79.
Four Readings Answer Different Questions
No numerical pass/fail limits are reproduced here because the supplied sources do not include the complete primary standards. Use the current standards, applicable instructions for use, qualified laboratory methods, and the facility water-management plan for limits and sampling frequency.
| Reading | Most Useful Signal | Relevant Finding | What It Cannot Prove |
|---|---|---|---|
| Hardness | Calcium and magnesium control | White or chalky deposits | Exact residue composition |
| Conductivity | Broad ionic load or treatment drift | Rings, haze, recurring deposits | Which ion caused the mark |
| Chloride | Corrosive exposure risk | Pitting or recurrent discoloration | That every brown mark is corrosion |
| Endotoxin | Pyrogenic contamination risk | Required by use, standard, or assessment | Cause of a visible spot |
Hardness Supports a Mineral-Deposit Hypothesis
Hardness testing is especially useful for removable white or chalky residue. Compare incoming water, the softener or pretreatment outlet, treatment output, and the actual washer final-rinse outlet. A satisfactory treatment-skid result does not rule out a downstream valve, tank, loop, pipe, or washer problem.
Softening primarily exchanges hardness ions such as calcium and magnesium. Reverse osmosis reduces a broader range of dissolved and suspended constituents through a membrane. Deionization removes charged ions through ion exchange. These processes are not interchangeable, and none guarantees suitable point-of-use water without correct operation, storage, distribution, and maintenance.
Conductivity Detects Drift but Not the Specific Contaminant
Conductivity is a broad indicator of ionic content. A change can reveal treatment breakthrough, contamination during distribution, or a difference between affected and unaffected outlets. It does not identify calcium, chloride, iron, detergent, or another constituent by itself.
Pair conductivity with the appearance, first affected stage, treatment history, and targeted analysis. A normal reading at one moment also does not explain an intermittent load pattern unless collection matched the equipment’s operating state.
Chloride Matters When Surface Attack Is Suspected
Chloride testing belongs in an investigation involving pitting, roughness, repeated discoloration, or concern about corrosive conditions. Metals such as iron, copper, or manganese may also be relevant when piping degradation, staining, or corrosion products are suspected.
A rust-colored mark is not proof that the stainless-steel instrument itself is rusting. It may be an iron-containing deposit from another component or the steam pathway. Determine whether it is raised, removable, adherent, or associated with material loss.
Endotoxin Is Not a Spot Test
Neither microorganisms nor endotoxins can be identified by color, texture, or removability. Endotoxin and microbiological testing may be required by the applicable standard, intended use, equipment instructions, or facility risk assessment, but a visible mark cannot substitute for those tests. Likewise, an acceptable endotoxin result does not explain a mineral or chemical film.
Samples Must Represent the Affected Point of Use
“Water quality” is a pathway rather than one building-entry sample:
Incoming potable water → pretreatment or softening → reverse osmosis or deionization where installed → storage → distribution → sink or washer → final-rinse outlet → boiler or steam generator → steam distribution → sterilizer
Quality can change at every transition. Storage may introduce stagnation or deposits. Distribution can contribute metals or scale. A washer may use different water qualities during different phases. Steam generation adds feedwater, boiler-treatment, carryover, piping, and condensate variables.
A facilities summary of ANSI/AAMI ST108 describes potable water, utility water, critical water, and steam or steam condensate as distinct categories. The required quality depends on intended use and the applicable device, chemistry, washer, disinfectant, sterilizer, and treatment-system instructions (HFM Magazine’s ST108 summary).
Drinking-water compliance therefore does not establish suitability for every device-processing stage. Mary Bridge Children’s Hospital reportedly removed trays and packets from circulation and sent them elsewhere for reprocessing after an out-of-standard specialized processing-water finding. Capacity was reduced and procedures were delayed or rescheduled even though municipal water reportedly continued to meet drinking-water standards. The report did not identify the failed parameter, document instrument spotting, or connect a particular water defect to visible marks (Mary Bridge incident report).
A useful sampling map includes the incoming supply, pretreatment outlet, treatment output, storage and distribution return, manual sink, washer inlet, washer final-rinse outlet, steam-generator or boiler feed, and point-of-use condensate. Include an unaffected comparison outlet when possible.
For every sample, record the exact outlet, date and time, equipment identifier, processing stage, operating state, upstream treatment, recent maintenance or sanitization, filter or resin changes, and associated loads. Collection container, flushing, preservation, transport, and analytical method must match the parameter.
A Questionable Tray Is Controlled, Not Wiped Into Service
A dry surface spot does not by itself prove microbial contamination, a wet pack, or a failed sterilization cycle. It does establish an unexplained post-processing condition that requires disposition under facility policy.
Preserve representative evidence before cleaning every surface. Photograph the mark and retain its association with the load, tray, washer, rack, sterilizer, and cycle. Document instrument types, materials, finishes, mark location, texture, removability, package condition, chemistry lot and dosing, maintenance history, and recent changes.
Do not release a tray merely because residue wipes off. If reprocessing is selected, route the item through the facility’s approved process and applicable instrument instructions rather than performing a local wipe-down. The investigation may also require holding related loads while the pattern is defined.
Remove an instrument from routine use for qualified evaluation when there is pitting, cracking, flaking, roughness, material loss, blocked lumens, a stiff joint, reduced movement, or damage to a working surface. A clean-looking exterior does not rule out deposits or corrosion inside a box lock or lumen.
Package integrity requires a separate decision. CDC guidance states that a sterilized package that is wet, torn, or punctured should not be used (CDC sterilizing-practices guidance). That rule does not mean every ordinary dry spot proves contamination; package moisture and damage have their own handling requirements.
Notify sterile-processing leadership and the facility functions required by policy. Depending on the pattern, that may include perioperative services, infection prevention, facilities, clinical engineering, quality or risk personnel, instrument specialists, the equipment manufacturer, the treatment provider, and a qualified laboratory.
Correct the Demonstrated Cause and Verify the Repair
Match corrective action to the evidence. Incorrect detergent or neutralizer delivery calls for calibration and dosing correction. Incomplete rinsing calls for restoration of flow, spray coverage, rack connection, programming, or loading. Treatment drift calls for maintenance and requalification of the treatment output. Distribution degradation requires attention to tanks, loops, stagnation, recirculation, piping, or corrosion.
A steam-pathway finding may require correction of feedwater treatment, boiler operation, blowdown, additives, filters, traps, regulators, separators, or piping. A drainage pattern may require changes to orientation, set design, loading, metal mass, wrap density, or drying performance. Instrument-specific damage requires manufacturer-directed or qualified technical disposition.
Do not purchase a softener, reverse-osmosis system, or deionizer solely from the spot’s appearance. Treatment selection should follow the verified contaminant, intended use, infrastructure, risk assessment, and applicable instructions.
After correction, repeat testing at generation and point-of-use locations, confirm equipment performance while operating, and inspect representative loads at the stage where marks first appeared. Compare affected and control loads and trend recurrence. Close the investigation only when analytical results, equipment findings, and subsequent loads support resolution.
FDA’s reusable-device reprocessing guidance addresses manufacturer validation and labeling for reusable-device instructions. It does not provide a spotting color chart or facility water-quality limits. Those requirements must come from current primary standards, applicable instructions, facility procedures, and qualified assessment.